Table of Contents
Introduction: Why Visual Inspection Fails for Modern Pulp‑Paper Production
Pulp Bleaching & Brightness: Secure Quality at the Fibre Source
Whiteness, Yellowness and OBA / FWA Fluorescent Whitening Agent Control
Opacity Measurement: Solve Print Show‑Through for Book, Notebook & Packaging Papers
Gloss Control for Coated Paper, Art Paper & Packaging Board
Recycled Fibre & Packaging Shade‑Drift Management for Sustainable Paper Manufacturing
3nh End‑to‑End Optical QC Solutions for Pulp & Paper Mills
Common Pulp‑Paper Measurement FAQs
Get Your Custom Technical Support & Sample‑Testing Service
Introduction: Why Visual Inspection Fails for Modern Pulp‑Paper Production
Pull a fresh ream of office printer paper from packaging. The top sheet shows crisp, clean white. Flip through ten sheets deeper into the stack, and you may spot a subtle yellowish shift barely detectable by human eyes. For luxury perfume packaging boxes with gold foil embossing, the white paperboard can shift to pale grey under retail store lighting, downgrading the premium shelf‑side visual impression for end‑consumers.
Paper’s optical performance is deceptively complex. Modern paper mills run high‑speed web‑lines, where raw wood fibre, recycled pulp, bleaching chemicals, fillers, coatings and process water combine within fractions of a second. Minor process fluctuations in pulp bleaching dosage, filler formulation, press‑roll pressure or coating weight will immediately shift whiteness, opacity and surface gloss across paper rolls and finished reams.
Human visual inspection has critical limitations for high‑volume pulp‑paper production:
Bright white paper surfaces create visual fatigue, making consistent subjective judgement difficult for QC inspectors.
Workshop lighting, retail‑store illumination and daylight change perceived colour drastically.
Subtle ΔE colour deviations invisible to eyes can trigger batch rejection, customer complaints and costly rework for converters, book printers and brand owners.
Objective, repeatable optical measurement delivers traceable numeric data to guarantee consistent quality roll‑to‑roll, ream‑to‑ream and box‑to‑box. That is where 3nh high‑precision spectrophotometers and gloss‑meter solutions add tangible value for pulp mills, paper‑making plants, packaging converters and brand‑quality teams.
Pulp Bleaching & Brightness: Secure Quality at the Fibre Source
Paper product quality originates in pulp‑mill bleaching workflows. Whether processing virgin wood fibre or post‑consumer recycled cardboard stock, pulp brightness is the foundational QC parameter before paper‑forming commences.
Pulp brightness is defined as the percentage of blue‑light reflectance measured at 457 nm wavelength on wet‑pulp pads or dried handsheets. Global industry relies on well‑recognised standards: ISO 2470 and TAPPI T452 define brightness‑testing protocols for pulp and paper substrates.
Even a‑0.5‑point loss in pulp brightness forces paper mills to consume excessive volumes of expensive optical dyes and whitening agents to hit target whiteness levels, raising chemical‑procurement costs and introducing extra colour‑variation risks in downstream production.
Fibre coarseness, moisture variance and uneven pulp‑sheet surfaces create measurement noise. Benchtop spectrophotometers fitted with large‑size measuring apertures average out surface irregularities to deliver stable, repeatable pulp‑brightness readings for laboratory QC workflows.
3nh benchtop spectrophotometers deliver high‑accuracy blue‑reflectance measurements inside mill‑laboratory environments. Pulp‑plant chemists monitor bleaching‑process efficiency in real‑time, optimising chemical consumption, cutting chemical waste, and locking in baseline pulp‑fibre quality before pulp enters paper‑making lines.
Practical tip: Always prepare handsheet test samples following ISO‑standardised preparation procedures; inconsistent sample moisture will introduce deviation in brightness‑test results.
Whiteness, Yellowness and OBA / FWA Fluorescent Whitening Agent Control
Modern office paper, marketing print substrates and premium packaging boards rely heavily on Optical Brightening Agents (OBA / FWA, Fluorescent Whitening Agents). OBAs absorb invisible ultraviolet UV radiation and re‑emit visible blue light, creating the visual illusion of brighter, cleaner‑looking white paper surfaces.
OBA‑modified paper creates major measurement challenges for quality‑control teams:
OBA fluorescence performance depends directly on UV‑energy content inside instrument light sources. Older‑generation measurement hardware outputs uncontrolled UV levels: too much UV artificially inflates whiteness index values; zero‑UV energy completely ignores OBA‑fluorescence effects. Either scenario generates non‑comparable, unreliable test data that cannot align with real‑world visual perception under D65 retail‑store lighting conditions.
To meet global buyer specifications such as CIE Whiteness W10 (D65/10° observer), instruments must support adjustable, automated UV‑control functions for paper‑grade testingTAPPI.
3nh high‑precision spectrophotometers integrate automated UV‑control hardware. Operators can rapidly toggle three working modes: UV‑Included, UV‑Excluded and UV‑Calibrated. This function outputs authentic CIE Whiteness Index, Tint value and Yellowness Index (YI), fully aligned with mill‑internal standards and international buyer specifications across North America, Europe and Asia.
Paper‑mill QC teams can quantify actual OBA‑additive performance, avoid over‑dosage of fluorescent whitening chemicals, and ensure cross‑lab data comparability between internal labs and external customer‑audit laboratories.
Opacity Measurement: Solve Print Show‑Through for Book, Notebook & Packaging Papers
Hold thin book‑paper against a bright window. Low‑opacity paper will show reverse‑side text bleeding through the sheet. Poor opacity ruins reading experience for book‑publishers, notebook‑manufacturers, catalogue‑printers and food‑packaging converters, degrading final product market perception.
Opacity quantifies how much light is absorbed when light transmits through paper sheets. Paper‑makers tune opacity outcomes by adjusting sheet thickness, fibre‑refining parameters and mineral‑filler dosage (titanium dioxide, calcium carbonate). Adding high‑cost mineral fillers boosts opacity but also increases raw‑material weight and overall production cost. Balancing opacity and manufacturing expense remains a persistent engineering challenge for paper‑mill process teams.
Standard ISO‑ and TAPPI‑compliant opacity testing requires dual‑sequence measurement:
Place the paper sample over a black light‑absorbing cavity or black ceramic tile for the first reading.
Measure the identical sample stacked over multiple reference white‑paper sheets or white‑reference tile for the second reading.
Instrument software automatically calculates ISO‑ or TAPPI‑standard opacity percentage values from the two‑point dataset.
3nh benchtop and portable spectrophotometers include built‑in automatic opacity‑measurement modes. QC operators complete paper‑stock testing within seconds. Mills achieve target opacity performance without unnecessary extra filler consumption, optimising material‑cost efficiency.
Portable units enable quick opacity spot‑checks on finished paper rolls and converted board stock outside laboratory environments.
Gloss Control for Coated Paper, Art Paper & Packaging Board
Colour performance tells only half of paper visual‑quality requirements. Surface gloss heavily shapes end‑user perception of coated‑magazine stock, high‑gloss packaging cartons, matte art‑paper and textured cardboard substrates.
High‑gloss magazine covers deliver sharp, vibrant printed visuals.
Matte photo‑art‑paper eliminates screen‑like glare and reduces eye‑strain for readers.
Mismatched gloss values on opposite sides of folding carton‑boards create inconsistent shelf‑appearance, making finished goods look low‑grade in retail‑store environments.
Paper‑industry standards define dedicated gloss‑measurement angles:
75° angle (TAPPI T480 / ISO 8254‑1) is the primary standard for coated‑paper and paperboard gloss testingISO.
60° angle applies for general matte‑coated and semi‑gloss paper grades.
20° angle is reserved for ultra‑high‑gloss coated‑paper surfaces.
3nh precision gloss‑meters deliver instant, accurate surface‑shine measurement results. Hand‑held single‑angle and multi‑angle gloss‑meter models enable QC personnel to scan moving paper webs, coated rolls and printed cardboard directly on‑site on the mill production floor. Operators detect uneven coating distribution before paper rolls are shipped to downstream converting partners, reducing conversion‑plant rejection rates.
Recycled Fibre & Packaging Shade‑Drift Management for Sustainable Paper Manufacturing
Sustainability targets drive massive adoption of recycled pulp, brown kraft paper and corrugated board globally. Recycled‑fibre raw‑materials bring inherent‑colour variation: residual printing‑ink traces, variable lignin content and mixed‑source waste‑paper batches cause unpredictable shade‑shift across production lots.
Visual comparison against physical paper‑reference swatches creates further pain points: physical paper standards degrade, yellow and soil during warehouse storage over time, breaking consistency between Asian mill‑production and European‑brand‑buyer approval workflows.
Spectral‑data tracking solves this pain‑point. 3nh portable spectrophotometers allow warehouse‑audit staff to inspect incoming paper‑rolls in‑situ within seconds. Inspectors capture CIELAB Lab* colour coordinates and Delta‑E (ΔE) colour‑difference values directly beside paper reels.
All spectral‑measurement data synchronises into 3nh SQCX professional colour‑management software deployed across pulp mills, paper‑factories, packaging converters and brand‑buyer quality‑departments. Digital‑colour‑standards replace ageing physical‑paper‑samples. Mill‑managers in Asia share complete digital spectral datasets with overseas purchasing‑teams instantly, eliminating slow‑physical‑sample‑shipping delays for batch‑approval cycles and speeding‑up order‑validation lead‑times.
3nh End‑to‑End Optical QC Solutions for Pulp & Paper Mills
The pulp‑and‑paper industry operates as a high‑volume, low‑margin business. Even one out‑of‑spec paper roll generates substantial material waste, production downtime and irreversible loss of customer‑trust.
From raw‑pulp bleaching control, through office‑paper and premium‑print‑paper production, to high‑gloss packaging‑board and recycled‑fibre‑box stock, 3nh delivers complete optical‑measurement toolkits covering the full paper‑manufacturing workflow:
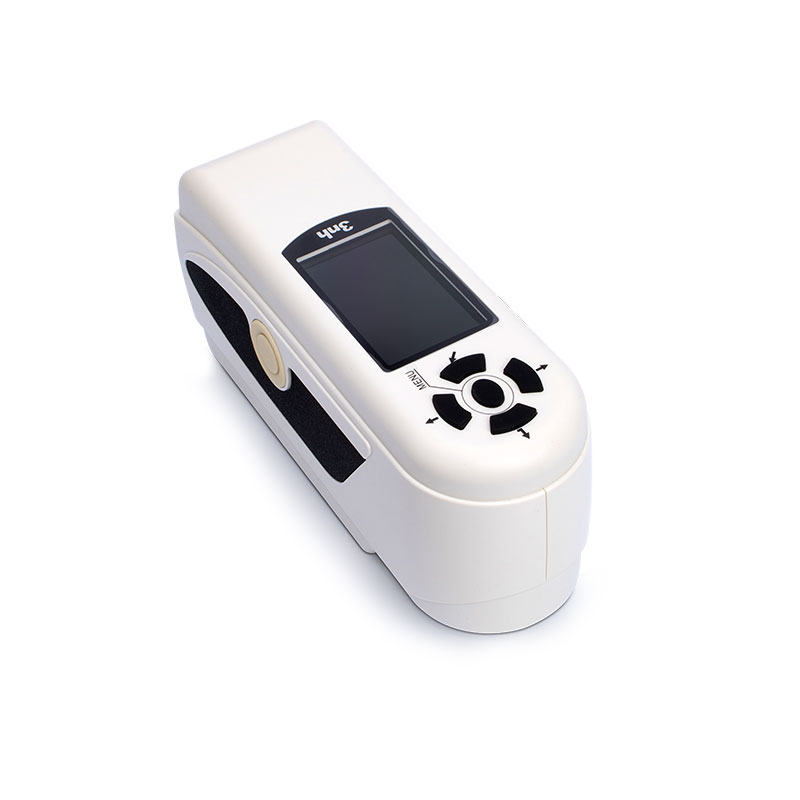
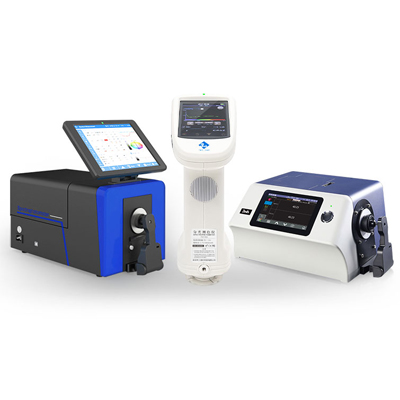
Benchtop spectrophotometers: Laboratory‑grade for pulp‑handsheet testing, whiteness‑OBA analysis, opacity‑index calculation, compliant with ISO 2470, TAPPI T452, CIE‑whiteness‑related standards. Large‑aperture options accommodate uneven pulp‑sheet samples.
Portable spectrophotometers: On‑roll spot‑checks for incoming raw‑material inspection, finished‑roll QC, warehouse‑audit and converter‑site quality‑verification.
Multi‑angle gloss‑meters: Production‑floor gloss QC for coated‑paper, art‑paper and packaging‑board, supporting 20°/60°/75° paper‑industry‑standard measurement angles.
SQCX colour‑management software: Centralised spectral‑data storage, digital‑standard library management, batch‑comparison, automated‑report export, cross‑site data‑sharing for global‑supply‑chain collaboration.
Real‑world use case: Multiple mid‑size Asian paper mills deployed 3nh benchtop spectrophotometers to monitor pulp‑brightness and OBA‑whiteness. Process‑engineers reduced excessive whitening‑agent consumption and lowered batch‑rejection rates for high‑grade office‑paper grades.
Common Pulp‑Paper Measurement FAQs
Q: Can visual light‑booth assessment replace spectrophotometer testing for paper‑grade quality control?A: Light‑booth visual assessment remains useful for final‑sample‑approval, but human‑vision cannot produce traceable numeric data. Spectrophotometers provide objective, repeatable datasets for process‑adjustment, supplier‑audit and cross‑continental‑supply‑chain‑communication.
Q: Why is adjustable UV‑control critical for OBA‑containing white‑paper?A: OBA‑fluorescence response changes with UV‑radiation levels. Without adjustable UV‑control, instrument‑readings deviate from real‑world retail‑lighting visual‑appearance, creating mismatches between lab‑test results and market‑product‑performance.
Q: Which instrument do I need for recycled kraft‑paper shade‑inspection?A: Portable d/8° integrating‑sphere spectrophotometers are well‑suited for on‑site recycled‑paper roll‑inspection, delivering Lab* and ΔE shade‑difference‑readings rapidly.
Get Your Custom Technical Support & Sample‑Testing Service
Every pulp‑and‑paper facility faces unique QC challenges: different fibre‑sources, OBA‑formula‑recipes, target‑paper‑grades and global‑customer‑standard‑requirements.
If you want to evaluate how 3nh spectrophotometer and gloss‑meter systems fit your mill workflows:
✅ Request free sample‑testing service for your pulp‑handsheets, finished‑paper or packaging‑board samples
✅ Receive application‑specific technical datasheets and standard‑compliance documentation
✅ Book a virtual‑demo with our optical‑engineering team
Contact us via service@3nh.com, share your paper‑grade specifications and existing QC‑pain‑points. Our Senior Optical Engineer Justin Lee and technical‑support team will reply with tailored recommendations for your pulp‑and‑paper‑colour‑gloss‑measurement project.
About the AuthorJustin Lee – Senior Optical Engineer, 3nhJustin owns over 15 years of R&D experience in colour‑measurement‑instrument technology and holds 8 patents for spectrophotometer optical‑system design. He collaborates closely with pulp‑paper‑manufacturers, packaging converters and global‑distributor‑partners to resolve real‑world optical‑quality‑control challenges across industries. Reach out to discuss your colour‑measurement‑project requirements at service@3nh.com.